
Lenntech R&D - Feasibility Testing
Lenntech R&D - Feasibility Testing
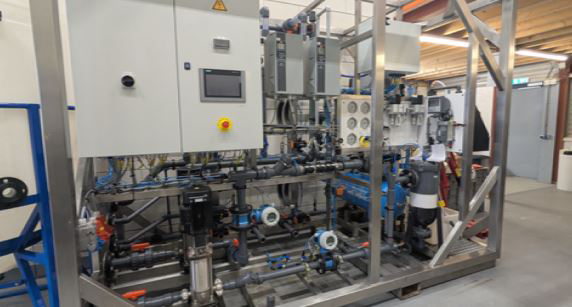
LTRD083 Ceramic UF Hollow Fiber UF/NF
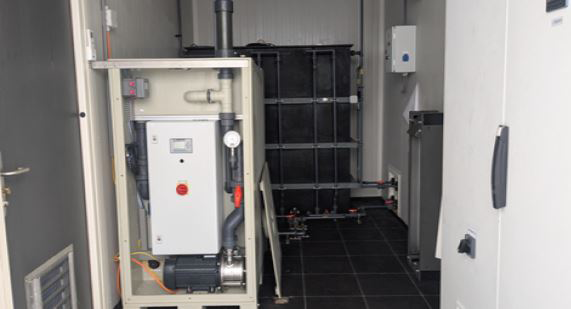
LTRD093 ED Electrodialysis
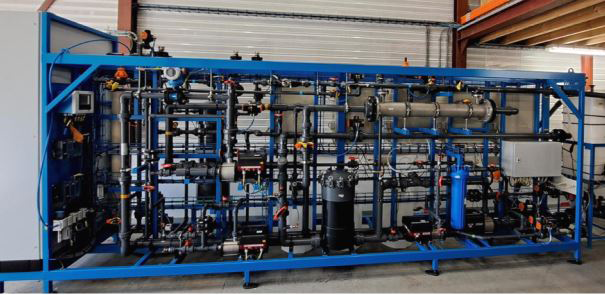
LTRD094 BPMED Bipolar Nenbrane Electrodialysis
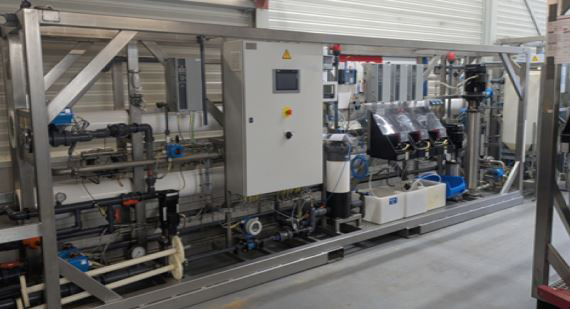
LTRD104 UHPRO Ultra High Pressure RO
 CHEMICAL PRODUCTION OF ACIDS AND BASES
Process Feasibility Assessment
Are you looking into building a full-scale separation system for your industrial plant? At Lenntech, we can offer you a feasibility study for a system that responds to your specific need. We accompany you through each step of the way, from conceptualization of your idea to the supply of the final integrated process.
Lenntech Water Treatment Solutions has 30 years of experience in the field of water treatment and separation processes. We practice at the cutting edge in the field of purification and recovery and implement innovative solutions to respond to our customer’s demands. To this aim, we supply a broad range of technologies to meet the desired effluent compositions and quality requirements. Key technologies, applications and industries include:

Pressure driven technologies
Electrically driven technologies
Ion exchange
Non-ionic sorption

Solutes separation or concentration
Solutes recovery
Stream deacidification or desalting
Brine minimization
Water reuse or discharge

Agriculture
Chemical
Energy
Food & Beverage
Pharmaceutical
Textile
SIGNIFICANCE
Our R&D feasibility study allows to:
- substantiate the performance of a proposed system
- collect operational and design parameters
- confidently move forward to the engineering of your full-scale system
- Recently, we observe a growing need of the industries for custom-made solutions targeting unconventional water streams. For these streams, moving directly towards a system design is too risky, as it involves a number of assumptions that still require validation.
- Assessing the feasibility of a process avoids future full-scale troubles, such as a non-adapted design, lack of performance, and additional financial costs.
APPROACH
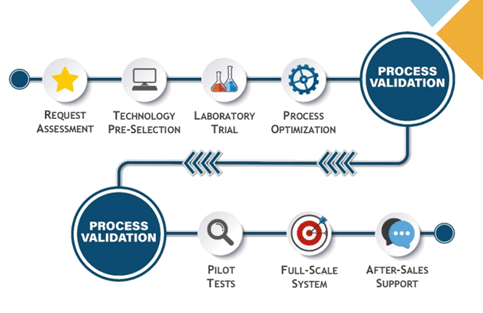
 Technology(-ies) Preselection
Together with you, our R&D team performs a preliminary assessment of your request based on your stream composition and main treatment objectives. By combining our expertise, scientific knowledge, and problem-solving mindset, an initial selection of most promising and technology(-ies) is made.
Laboratory Proof-of-Concept
During our laboratory proof-of-concepts, we conduct experiments on bench-scale set-ups to assess the feasibility of the preselected separation processes, and to optimize the process before moving to larger-scale installations. This evaluation is preferentially carried out on a representative sample of the industrial stream. This way, we can evaluate the need for pre- or post-treatments, and anticipate potential difficulties linked to the presence of other solutes or suspended solids.
Pilot-scale Assessment
When the outcomes of the laboratory Proof-of-Concept are favorable, pilot-scale tests allow to evaluate the scalability of the separation process before proceeding with the full-scale design. This is an important step in the treatment assessment, during which we validate the process configuration and design parameters. From there and together with our process and project engineers, we make a detailed offer for your full-scale plant.
Full-scale system
LAB & PILOT FACILITIES
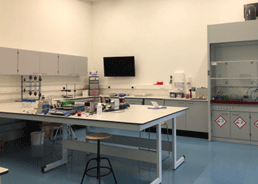
Testing laboratory
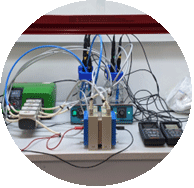
(Bipolar membrane) Electrodialysis
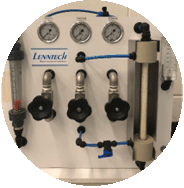
Ultrafiltration / Nanofiltration
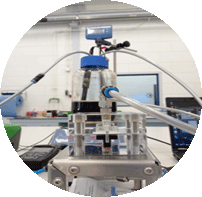
Membrane distillation
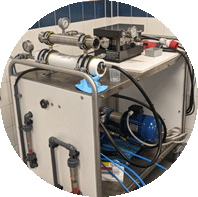
Spiral-wound reverse osmosis
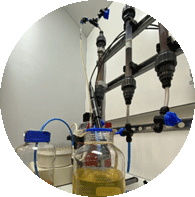
Ion exchange
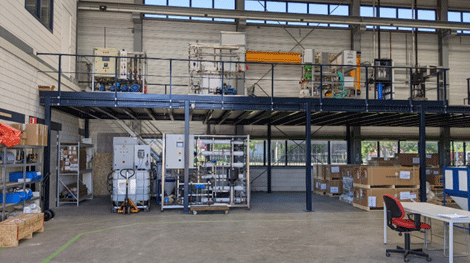
Storage Test Equipment
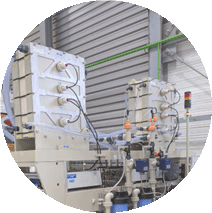
Electrodialysis
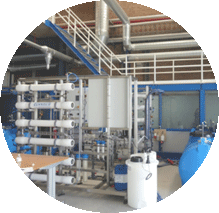
Nanofiltration and reverse osmosis
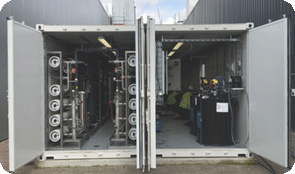
Integrated system
Separation and Concentration Purification Request with Lenntech
for your industrial separation, filtration, concentration, and purification case studies.
In the past Lenntech has been asked to investigate, test, resolve and propose solutions to these types of challenges:
- Remove divalent salts (Ca, Mg) from industrial process water.
- Concentrate Sodium Chloride (NaCl) brine from 215 to 245 g/liter
- Purify and concentrate hydrogen peroxide (H₂O₂)
- Auto-regenerate an activated carbon bed
- Concentrate C5/C6 sugars in a saline and acidic solution
- Reduce salts to prevent too frequent Ion Exchange bed regeneration
- Ethanol dehydration
- Adsorption of Stevia Glycoside, Steviol, Stevidin and Flavonoids substance removal
- Separate chlorates from feed water in the food industry.
- Remove humic substances from surface water
- Ammonium removal from fertilizer wastewater
- Ethylene Glycol rejection
- Heavy metals filtration (Molybdenum MO, Copper CU, Lead Pb, Zinc Zn) - Extraction of metal oxides
- Color removal from textile run-off water
- Purification and Recycling of Membrane Bio Reactor (MBR) effluent.
- Treatment of persistent organic pollutants (Pops)
- Desalination of organic liquids
- Convert Sodium Sulphate (Na₂SO₄) into Caustic (NaOH) and Sulphuric Acid (H₂SO₄)
- Zero Liquid discharge (ZLD) of factory outlet
- Dehydration of mixture of organic acids
- Non-biodegradable COD oxidation in leachate water after biotreatment of biomass
- Lithium extraction from mining water
- Protein recovery - downstream Bioprocessing bacteria, enzymes, chloroplasts
- Dissolved Solids removal (TDS & TSS) in ultrapure water
- Colloids removal measurement (SDI)
- Controlled ion exchange column trials evaluating; loading, rinse and regeneration in a controlled environment.
- Cooling tower blowdown water purification preventing chemical precipitates
- Neutralisation of acidic streams
- Oxidation of halogenated hydrocarbons
- Sugar cane & juize decolorization, Citrus debittering, juice deacidification, sugar demineralization
- Biofouling and scaling prevention on membranes
- Desalinate water with high Silica content
- Treatment of spent caustic
- Solid–liquid separation and mineral processing
- NOM >90% and atrazine reject elimination
- PFAS removal systems for well water
- Heap Leaching - Cyanide/Ammonia/Alkali/Acid chemical leaching ore (gold, silver, nickel and uranium)
- Phosphorus removal system for liquid manure
- Manganese Removal from Drinking Water Sources
- Selective Sodium removal from horticulture/agriculture recycle water
- Lowering the concentration of salts or solvents from solutions containing proteins, peptides, nucleic acids, and other biomolecules
We provide a first theoretical analysis of concept for free if we see possibilities for treatment.
As second step we can do a lab scale/bench sale test with a sample for a proof of concept (POC) feasibility study providing budget costs and parameters after which we could scale-up the process/technology to pilot and or full-scale.
For above questions the Lenntech R&D application center has researched and developed unique technologies and processes either individually or in combination using amongst others:
Membrane Separation - Nanofiltration (NF) – (Ceramic) Ultrafiltration (UF) – Ion Exchange (IX) – Vacuum Membrane Distillation (VMD) – Pervaporation (PV)– Zeolite adsorption – Electrodialysis (ED) – Granular Activated Carbon (GC) – Bipolar Membrane Electrodialysis (BPMED) – Advanced Oxidation (AO) – Wet air oxidation (WAO) - Evaporation and Crystalisation - physiochemcial Coagulation and Flocculation – Precipitation and Sedimentation – Electrodialysis Reversed (EDR) – Electro Coagulation (EC) – Cross-flow Microfiltration (MF) - Continuous Electrodeionization (CEDI) - Reverse Osmosis (RO) - Multiple Effect Distillation (MED) - Mechanical Vapor Recompression (MVR) – Vapor Compression (VC) – Osmotically assisted RO (OARO) - Multi Media Filtration (MMF) – Dissolved Air Flotation (DAF) Ultraviolet Oxidation (UVO) – Hollow fiber NF/RO – Tubular RO - Cationic and anionic ion exchange membranes - Electrodeionization (EDI) - Advanced photo oxidation processes (APOP) – Absolute Filtration – Centrifugation - Molecular weight cut-off (MWCO) – Electrochlorination - Capacitive deionization (CDI) - Forward osmosis (FO) - Eutectic Freeze Crystallization (EFC) – Ultra high pressure RO (UHPRO) - Fixed-Bed Adsorption Reactors - Neutralization – Scrubbing - Stripping - Spay drying - Lime softening - Humidification/dehumidification - Diafiltration - Membrane crystallization (MCr) - Liquid Liquid extraction - solid phase nucleation in supersaturation - Pressure Retarded Osmosis (PRO) - Osmotic Distillation (OD) - Gravity Separation - Electrophoresis - Fractionation - Chromatography - all part of our Research and Development engineering tools.
For more information or quotation, please contact us:  Feedback Form or call us on +31 152 610 900